Bulk oil buyers rarely judge a supplier by brochure language. They look at the sunflower oil production process because process discipline affects yield, quality consistency, traceability, and delivery reliability. For importers, food manufacturers, and distributors, understanding how sunflower oil is produced is not technical background - it is part of supplier evaluation.
Sunflower oil is a straightforward product on paper, but the commercial result depends on how well each production stage is controlled. Seed condition, extraction method, refining parameters, filtration, storage, and shipment handling all influence the final oil specification. A supplier with real manufacturing capability should be able to explain these stages clearly and without overstating them.
What the sunflower oil production process includes
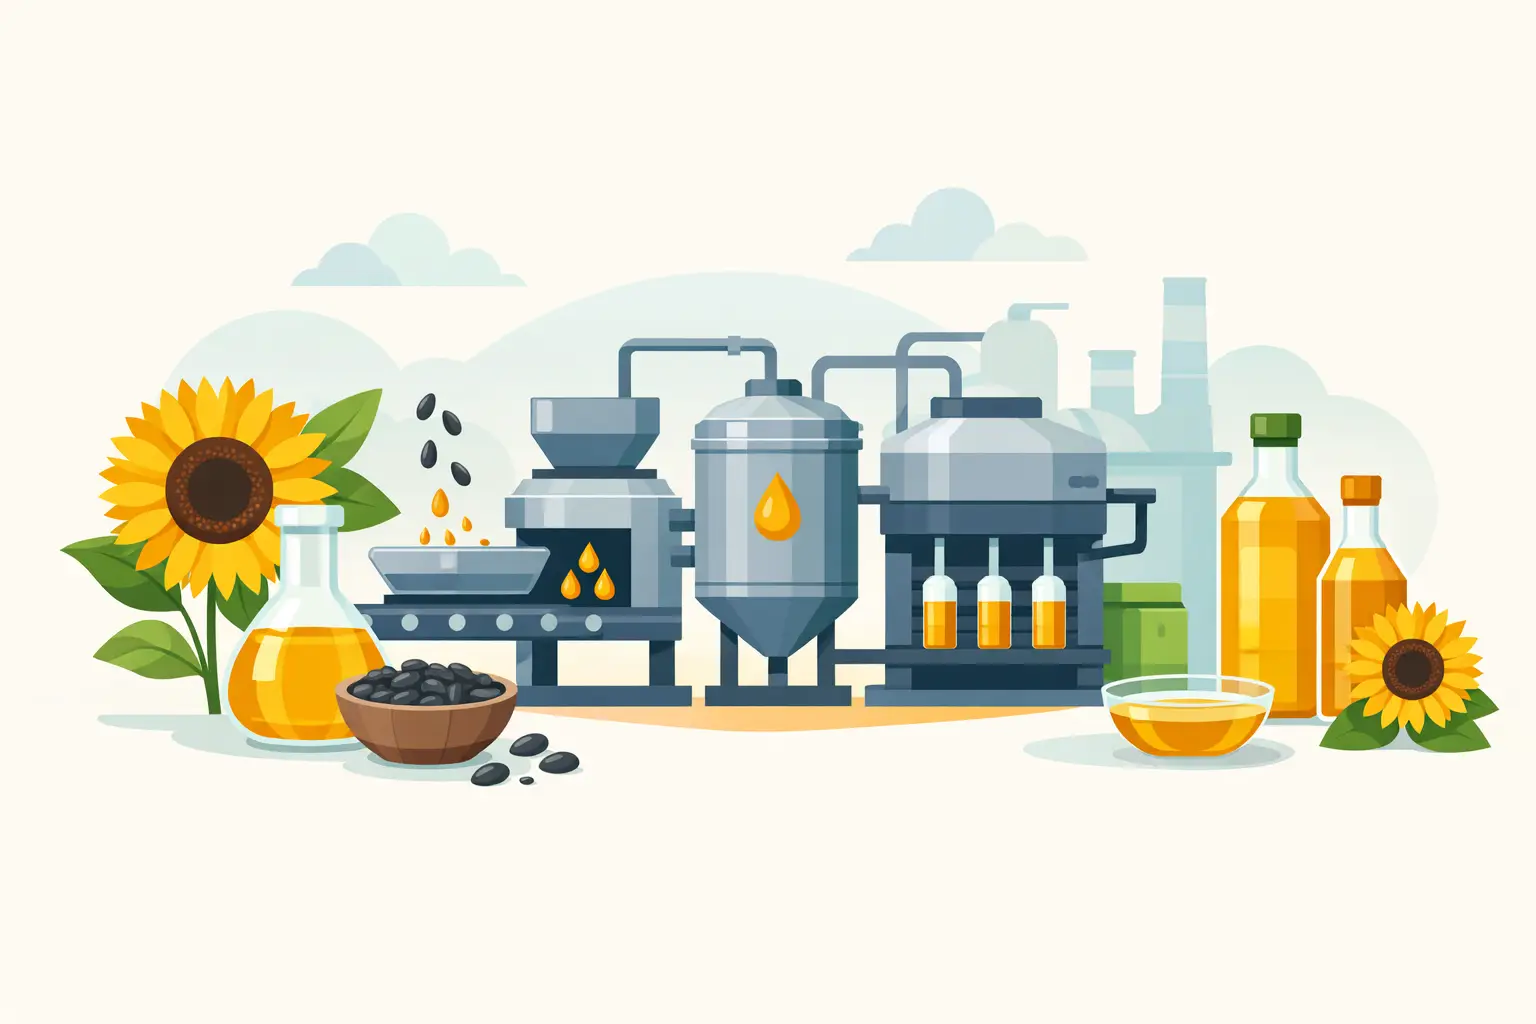
The sunflower oil production process begins long before oil enters a storage tank. It starts with raw material selection and ends with finished oil prepared for bulk dispatch or further packaging. In industrial terms, the main stages are seed reception, cleaning, conditioning, dehulling when required, mechanical pressing or extraction, crude oil clarification, refining, filtration, storage, and loading.
Not every plant uses the exact same configuration. The differences usually come down to intended product grade, plant capacity, customer specification, and whether the producer focuses on crude sunflower oil, refined sunflower oil, or both. That is why procurement teams should not look only at whether a supplier produces sunflower oil, but how the process is managed and where quality is verified.
Seed reception and raw material control
Production quality starts with the seed. Incoming sunflower seeds are checked for moisture, foreign matter, damaged kernels, and overall condition. If this step is weak, downstream efficiency suffers. High impurity levels reduce extraction performance, increase equipment wear, and can affect oil quality.
For commercial buyers, this matters because raw material variability shows up later as inconsistency in color, odor, free fatty acid level, or refining loss. Producers operating in a major sunflower-growing region have an advantage only if they combine origin access with proper intake control. Agricultural relevance alone is not enough.
After reception, seeds typically move through cleaning equipment to remove dust, stones, metal particles, stalks, and other foreign material. This is a practical step, not a minor one. Clean feedstock protects machinery and supports stable oil recovery.
Preparation before extraction
Once cleaned, the seeds are prepared for oil recovery. Depending on the plant setup and product target, this may include drying, cracking, dehulling, grinding, and conditioning through heat treatment. The purpose is to create a material structure that allows efficient oil release.
Dehulling is one of the points where process decisions vary. Removing hulls can improve meal quality and affect extraction performance, but it also adds another processing stage. Some producers dehull more aggressively, while others balance throughput, cost, and product requirements differently. For buyers, this is one of many examples where the best process is not universal - it depends on the end market and specification priorities.
Conditioning is equally important. Proper temperature and moisture adjustment support pressing efficiency and help maintain process stability. If conditioning is inconsistent, oil yield may drop and the crude oil can contain more impurities, which raises the refining burden later.
Pressing and extraction in the sunflower oil production process
At the core of the sunflower oil production process is extraction. In many industrial plants, seeds or prepared sunflower material first go through mechanical pressing. This stage removes a significant portion of the oil and produces crude pressed oil along with press cake.
Mechanical pressing is valued for its directness and established industrial use. However, pressing alone may leave residual oil in the cake. For producers seeking higher total recovery, an additional extraction stage may be used. This improves yield, but it also adds process complexity and requires tighter operational control.
From a buyer perspective, extraction choice affects more than output volume. It can influence crude oil characteristics, production economics, and the supplier’s ability to meet large-volume contracts competitively. A manufacturer supplying food industry customers at scale must balance efficiency with specification control.
After extraction, crude oil is not yet ready for many commercial food applications. It still contains suspended solids, phospholipids, waxes, pigments, free fatty acids, and other natural compounds that need to be reduced or removed depending on the final product grade.
Crude oil handling and clarification
Fresh crude sunflower oil is usually routed through settling, screening, or filtration systems to remove solid particles. Early clarification protects downstream refining equipment and improves process consistency. This stage may appear routine, but poor crude oil handling can create avoidable losses and quality deviations.
Temperature control also matters. Oil that is overheated or held improperly can deteriorate. For B2B buyers, this is one of the practical reasons supplier credibility depends on plant operation, not just nominal capacity. A large production line has limited value if handling standards are weak between extraction and refining.
Refining for food-grade specifications
Refining is the stage that converts crude sunflower oil into a more commercially suitable edible oil. Depending on the required final specification, the process may include degumming, neutralization, washing, bleaching, winterization, deodorization, and final filtration.
Degumming removes phospholipids and related compounds. Neutralization addresses free fatty acids. Bleaching reduces color bodies and helps remove trace contaminants. Deodorization removes volatile compounds that affect smell and taste. Winterization is especially relevant for sunflower oil because wax content can affect clarity under lower temperatures.
This is where buyers should pay attention to the difference between merely refined oil and well-refined oil. Over-processing can reduce desirable quality characteristics or create unnecessary losses. Under-processing can leave the product outside customer requirements. The right refining approach depends on the intended destination market, storage conditions, and food application.
For example, oil destined for further industrial use may be supplied to a different specification than oil prepared for direct food packing. A competent producer should align refining depth with contract requirements rather than applying a one-size-fits-all model.
Quality control and specification consistency
In edible oil trade, consistency often matters as much as headline price. Buyers need confidence that one shipment matches the next within agreed parameters. That makes quality control a production function, not just a laboratory function.
During and after production, sunflower oil is commonly monitored for moisture, impurity level, acid value, peroxide value, color, odor, and other relevant indicators. The exact test profile depends on whether the oil is crude or refined and what the customer requires. What matters commercially is not just having test results, but maintaining repeatability through controlled production.
This is one reason experienced manufacturers are valued in the market. Plants with long operational history usually have a clearer understanding of seasonal raw material variation, process adjustment, and shipment preparation. EKOBIOTEK, operating from Kherson with production history dating back to 2003, reflects the type of manufacturing continuity many procurement teams look for when evaluating supply partners.
Storage, tank management, and dispatch
Finished oil quality can still be compromised after refining if storage and loading are poorly managed. Oil is typically held in dedicated tanks under controlled conditions before shipment. Tank cleanliness, segregation, temperature management, and turnover discipline all affect product integrity.
For bulk buyers, this part of the chain is not secondary. Cross-contamination risks, sediment formation, and shipment delays often emerge at storage and dispatch rather than in extraction. A serious producer treats logistics readiness as part of manufacturing performance.
Before loading, the oil may pass through final filtration and release checks. Then it is dispatched according to the agreed format, whether bulk tanker, flexitank, containerized volume, or another commercial arrangement. The process must support documentation accuracy as well as physical product quality.
Why process transparency matters to buyers
A supplier does not need to turn every commercial discussion into an engineering lecture. But buyers should expect clear answers on raw material handling, extraction method, refining scope, quality controls, and shipment preparation. Vague language is usually a warning sign.
The sunflower oil production process is not complicated in theory. The challenge is maintaining control at industrial scale, across changing crop conditions and ongoing delivery commitments. That is where producer identity matters. A specialized manufacturer has more at stake in process stability than a trading intermediary.
For procurement teams, the practical question is simple: can the supplier show a repeatable production system that supports your volume, specification, and continuity needs? If the answer is yes, the discussion moves from commodity price alone to long-term supply confidence.
When evaluating sunflower oil supply, process clarity is one of the few signals that remains useful after marketing language is stripped away.